If you’ve ever wondered how that lightweight, super-strong part on your new sports bike, wind turbine blade, or even your favorite laptop case comes to exist, the answer often boils down to carbon fiber composites. As someone who’s spent the last decade supplying high-grade carbon fibers to aerospace, automotive, and industrial clients, I get asked this question all the time. It’s not just about mixing two materials together—this is a precise, multi-step process that balances raw material quality, environmental control, and meticulous craftsmanship to deliver a product that’s stronger than steel, half the weight, and tailor-made for modern engineering. Let’s break down the manufacturing process, step by step, as I’ve seen it play out in the facilities we partner with every day. Carbon Fibers

It starts long before we ever touch a spool of carbon fiber. The first core component of any carbon composite is, well, the carbon fiber itself. The base material here is not some rare or futuristic substance—it’s polyacrylonitrile, or PAN, a synthetic polymer that’s widely produced across the globe. But not all PAN is created equal. For high-performance composites, the PAN has to be pure, with a specific molecular structure that will hold up through the intense processing it’s about to undergo. The raw PAN first comes as fine, spun filaments, each only a fraction of the width of a human hair. These filaments are bundled together into large tows—think of them as thick “threads” of hundreds or thousands of individual fibers. At this stage, we’re already at the supplier level: our job is to source only PAN that meets strict tensile strength and uniformity standards, because even a tiny imperfection in the base material will show up as a weak spot in the final composite part. That’s why we work closely with mills to audit every batch of PAN before it moves to the next stage.
Once the PAN filaments are ready, they undergo a transformation that turns them from ordinary plastic into pure carbon. This is called carbonization, and it’s the most critical (and energy-intensive) step in the entire process. The tows of PAN are fed into giant ovens, called carbonization furnaces, in a continuous line. The air inside these ovens is carefully controlled—we use nitrogen gas to eliminate oxygen, because if the PAN burned, it would turn to ash instead of carbon. The temperature inside the furnace is staged, starting at around 200°C (392°F) and climbing all the way up to 1,500°C to 3,000°C (2,732°F to 5,432°F) as the filaments move through. At these extreme heats, the non-carbon elements in the PAN—hydrogen, oxygen, nitrogen—are burned off or removed as gas, leaving only tightly packed carbon atoms arranged in thin, strong crystalline structures. The result here is raw carbon fiber filaments, which are much stronger and stiffer than the original PAN, but also very brittle. We don’t supply this raw carbon fiber to our clients, though—we ship it with a protective surface treatment, which brings us to the next stage: surface modification.
Raw carbon fiber is smooth and chemically inert. That means if we just send a spool of it to a manufacturer, the resin we’ll mix it with later won’t stick properly. The composite’s strength depends on a tight bond between the fiber and the resin, so we have to treat the fiber’s surface to create tiny, reactive sites that the resin can grip. This step, called sizing or surface oxidation, is a delicate balance. We use processes like electrolytic oxidation, where a mild electrical charge is applied to the fiber as it moves through a bath, or gaseous oxidation in a low-temperature chamber, to etch tiny microgrooves and functional groups onto the fiber surface. We also apply a thin sizing coating at the end of this process—usually a water-based epoxy or polyurethane—that protects the fragile carbon filaments from rubbing together and breaking during handling, shipping, and prepping for composite manufacturing. This is where our role as a supplier really matters: we test every batch of sized carbon fiber to measure its surface roughness, adhesion strength, and tensile integrity to make sure it will work for our clients’ specific applications. For a wind turbine blade, for example, we need fiber that has a very high shear strength between filaments, while for a medical prosthetic part, we prioritize fiber that won’t shed particles and is easy to work with in high-precision layup.
Now, once the sized carbon fiber is in the hands of a part manufacturer, the next stage is forming the composite structure itself. This is where the carbon fiber meets the resin, the second core component. Resin is a polymer that acts as a matrix, holding the carbon fibers in place, distributing load across the entire part, and protecting the delicate fibers from impact, moisture, and damage. There are two main types of resin used in carbon composites: thermoset, which is the most common for high-performance parts, and thermoplastic, which is newer and gaining traction for its ability to be reshaped after curing. Thermoset resins like epoxy are mixed with a hardener, then start to cross-link and cure into a rigid, permanent shape when heated or exposed to UV light. Thermoplastics, on the other hand, stay as a solid until heated to their melting point, then cool into a hard shape without needing a chemical reaction.
The way the carbon fiber and resin are combined depends on the final part. The most common method for low-to-medium volume, high-precision parts is hand layup, where technicians layer sheets of woven or unidirectional carbon fiber (sheets where all fibers run in the same direction, ideal for part-specific strength) into a mold, brushing resin over each layer by hand. For higher-volume applications, like automotive body panels or bicycle frames, manufacturers use automated processes like filament winding, where a machine winds continuous carbon fiber impregnated with resin around a rotating mandrel, or automated tape laying, which uses a robotic arm to place pre-impregnated carbon fiber tape exactly where it’s needed with consistent pressure. Another method popular for large parts, like wind turbine blades, is resin transfer molding (RTM), where a dry fiber preform is placed in a closed mold, and liquid resin is injected under pressure to flow evenly through the fiber, eliminating air bubbles that would weaken the part. No matter the method, the goal is the same: to lay up the carbon fiber with a specific orientation. That’s because carbon fiber is strongest along the direction the fibers run, so engineers design the layup to match the loads the part will face. For example, a wind turbine blade layup will have more unidirectional fibers running along the blade’s length to handle the force of wind, while woven fibers are used for the outer layer to resist impact from debris.
Once the fiber and resin are arranged in the mold, the part moves to the curing stage, where the resin hardens into a solid composite. For thermoset resins, curing usually happens in an oven or an autoclave— a pressurized oven that applies both heat and vacuum pressure to the part. The vacuum removes any trapped air between the layers, and the pressure presses the layers together, ensuring a strong, void-free bond between fiber and resin. Curing times vary wildly: small parts like bike handlebars might take an hour or two at 120°C to 180°C (248°F to 356°F), while large wind turbine blades can take several hours or even a full day to cure at a steady temperature. For thermoplastic composites, curing is simpler in some ways, but requires higher temperatures, often over 200°C (392°F), to melt the resin and bond the layers. Thermoplastics also can be “recycled” more easily than thermosets, which is a big selling point for automotive and aerospace manufacturers focused on sustainability.
After curing comes finishing, the stage that turns a rough, rigid composite block into a usable part. This involves trimming excess material from the edges, drilling holes for bolts or fasteners, sanding the surface smooth, and applying a protective coat or paint. For parts that need high precision, like aerospace components, CNC machining is used to cut the composite to exact dimensions, since the material is hard and can crack if cut incorrectly. Quality control is woven into every step here too—we partner with our clients to test parts for void content, tensile strength, and durability, because even a tiny void from trapped air can lead to catastrophic failure under load. As a supplier, we also provide technical support to help our clients choose the right fiber type and sizing for their specific application, whether that’s a race car part that needs maximum strength-to-weight ratio or a consumer electronics case that needs to be scratch-resistant.
Over the last few years, the process has evolved a lot. New methods like additive manufacturing (3D printing) with carbon fiber reinforced polymers are starting to open up new possibilities for complex, custom parts for aerospace and medical devices, cutting down on waste from traditional layup methods. There’s also a big push toward more sustainable carbon fiber manufacturing, with mills investing in processes that use less energy for carbonization, or even producing carbon fiber from recycled PAN or recycled carbon fiber scrap. That’s a trend we’re proud to be part of: more clients are asking for low-carbon-footprint composite materials, and we’ve expanded our product line to include fibers made with 30% less energy during production, without sacrificing performance.
What’s always stuck with me about this process is that it’s equal parts science and art. You can have the best raw materials and the most precise machinery, but you need skilled technicians who understand how to handle the fragile fiber, how to adjust resin mixes for different temperatures, and how to spot a minor flaw before it becomes a big problem in a final part. As a carbon fiber supplier, our job isn’t just to send spools of fiber down the road—it’s to be part of that process, helping our clients navigate the nuances of composite manufacturing, from choosing the right tow size to making sure the surface treatment will work for their specific part.
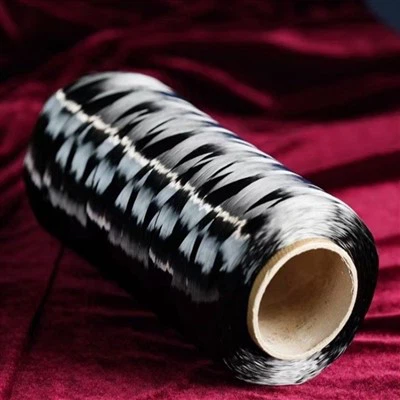
Whether you’re an engineer designing a next-generation wind turbine, a bike builder crafting a race-winning frame, or a product developer creating a lighter, stronger consumer electronic case, carbon fiber composites are likely going to be part of your future. The manufacturing process is complex, but it’s also endlessly adaptable, and as we continue to innovate, it’s only going to become more accessible and more sustainable. If you’re working on a project that requires high-quality carbon fiber, we’re here to walk through the details with you—from selecting the right fiber to specs to troubleshooting any part of the composite manufacturing journey.
Carbon Fiber Composite Materials References
- Chaudhary, S. (2020). Carbon Fiber Composites: Manufacturing, Properties, and Applications. CRC Press.
- Mallick, P. K. (2018). Fiber-Reinforced Composites: Materials, Manufacturing, and Design. CRC Press.
- Carbon Fiber Manufacturing Association. (2022). Global State of Carbon Fiber Production and Supply.
- Bradley, A. (2021). Surface Modification of Carbon Fibers for Composite Bonding. Journal of Composite Materials.
Jiaxing Rongjin Intelligent Technology Co., Ltd.
As one of the most professional carbon fibers suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please rest assured to buy high quality carbon fibers in stock here from our factory. Contact us for quotation.
Address: No.503, Building 1, Xicundai Road 228, Honghe Town, Xiuzhou District, Jiaxing City, Zhejiang Province, China
E-mail: vivi@rongjinsmart.com
WebSite: https://www.carbonfibers-china.com/
